

3-phase Separator for Kazakhstan Oil Refinery
Updated: Aug 24
Project Background
This project targets equipment renewal for an operating oil refinery in Kazakhstan. The original ageing three‑phase separator suffered from degraded separation performance, unstable level control and frequent freeze‑up risks during long, frigid local winters. The refinery needed a reliable horizontal three‑phase separator to replace the outdated unit, to realise stable separation & accurate metering of formation fluids (oil, gas and water phases) under harsh cold‑climate operating conditions.
The customer set a tight delivery timeline of only 3 months. The new separator must survive cold continental winters, with complete freeze‑protection packages for the vessel, instruments, valves and process piping to avoid medium solidification and guarantee non‑stop refinery operation in low‑temperature seasons.
Equipment Introduction
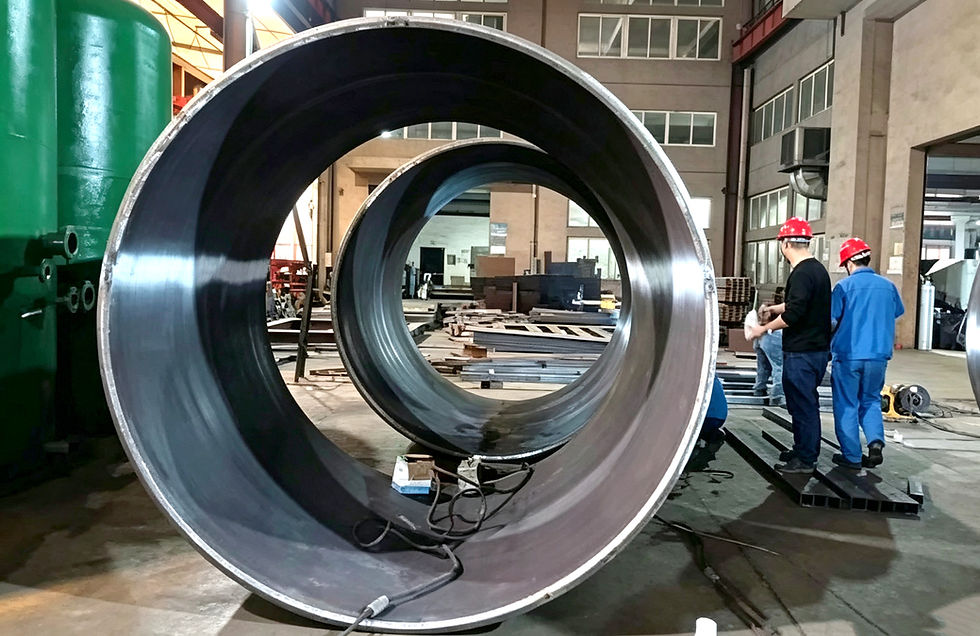
A horizontal three‑phase separator was selected for this refinery renovation project. Horizontal configuration offers convenient transportation, installation and routine production measurement, which perfectly matches site renovation requirements.
Key internals include inlet distributor, coalescing plates, defoamer and demister. When formation fluid flows into the vessel, inlet distributor completes initial gas‑liquid separation. Droplet‑laden gas passes through coalescing plates, defoamer and demister for further purification before dry gas discharges via gas outlet. Pneumatic control valves on gas piping stabilise working pressure inside the pressure vessel.
Under gravity and oil‑water density difference, free water settles to the bottom, while crude oil floats upward. Oil flows over the oil‑water baffle into the oil chamber. Float‑type level controller modulates oil discharge valve to stabilise oil‑phase level; the oil‑water interface controller actuates the water drain valve to keep a steady oil‑water interface. The unit achieves continuous three‑phase separation and accurate production metering for refinery crude pre‑treatment.

Cold‑climate Customisation (Kazakhstan Winter‑proof Design)
To adapt to Kazakhstan’s severe winter conditions, special winterisation & anti‑freezing measures were fully integrated into the design:
Full‑scope thermal insulation & electric heat‑tracing system: Vessel shell, all process pipelines, level transmitters, float‑type level controllers, drain valves and instrument manifolds are equipped with electric heat tracing plus external insulation cladding, preventing water and crude fractions from freezing in cold weather.
Low‑temperature‑resistant material selection: Vessel shell, nozzles and critical welds adopt low‑temperature impact‑tested materials, suitable for outdoor winter ambient conditions.
Optimised control logic for cold‑site operation: Level & pressure control loops are calibrated for low‑temperature environments to eliminate false‑level signals caused by cold‑affected instruments.

Manufacturing & Quality Control
Against the tight 3‑month project schedule, our factory implemented strict quality management across every production procedure: raw‑material screening, low‑temperature material verification, parameter tuning, welding inspection, NDT test, insulation and heat‑tracing assembly. All technical requirements for pressure‑vessel and cold‑climate customisation were strictly followed, with several indicators exceeding the customer’s original technical specifications.
Every component including vessel internals, pneumatic control valves, float‑type level controllers, oil‑water interface controllers and the complete freeze‑protection package went through full‑function pre‑commissioning before delivery.

Project Outcome
After 3‑month intensive fabrication and testing, the custom‑built horizontal three‑phase separator was completed and rolled off the production line on schedule. All pressure‑vessel inspections, separation‑performance tests and anti‑freezing function verification passed customer acceptance.
Installed as replacement for the old unit at Kazakhstan oil refinery, the separator runs stably year‑round. The winter‑proof package effectively eliminates freezing risks for vessels, instruments and pipelines in cold seasons. Stable oil‑gas‑water separation and accurate metering have been achieved, supporting continuous refinery production. The customer gave high evaluation on product quality and site performance, and expressed intention for long‑term future cooperation.

Our Capability
Winning Petro deliver custom‑engineered three‑phase separators for oil refineries and oil‑field sites worldwide. Our scope covers standard units as well as cold‑climate‑adapted versions with complete freeze‑protection packages for high‑latitude regions such as Kazakhstan.
Should you have any requirements for three‑phase separation equipment, please feel free to contact us. We are ready to provide professional technical support and customised solutions at your earliest convenience.


Comments